

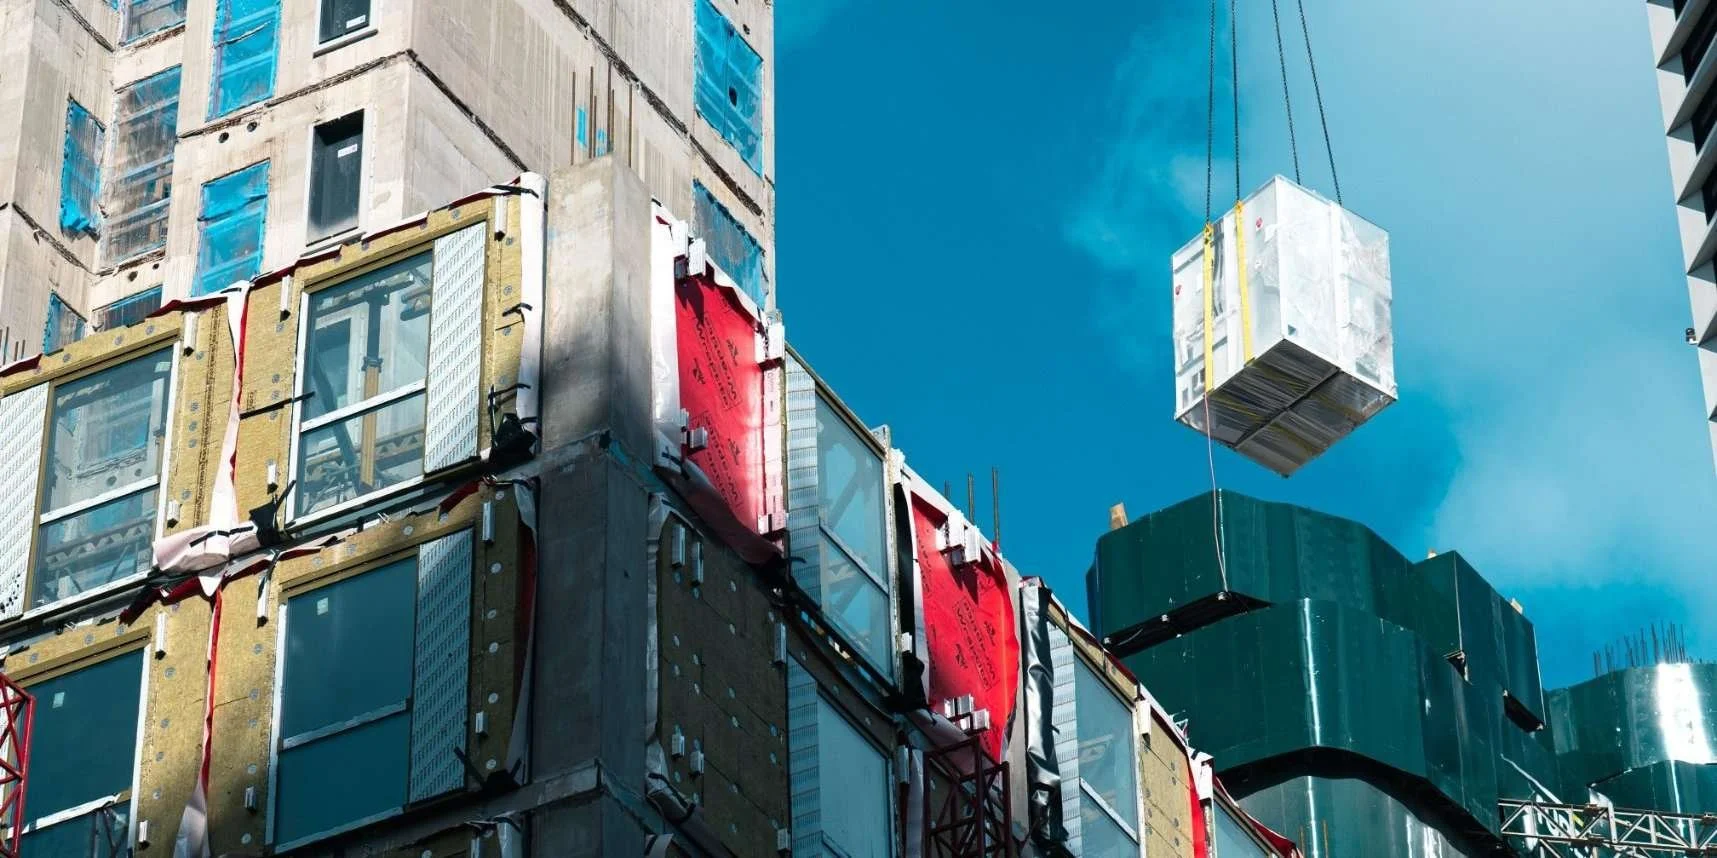
Twenty storeys of student accommodation are going up in Macquarie Park at roughly a floor a week. Build Australia reported in September 2026 that the tower had reached level 12, thirteen weeks after the first modules were craned into position on 12 June 2026. Its 528 units are being built in China by volumetric modular provider Freecity and delivered through modular integrator Space Labs Australia, each one arriving fitted out, facade included. Build Australia reports it is expected to be Australia’s tallest volumetric modular building.
A floor a week looks like the answer to the housing shortage. It is a stacking rate. The program behind it started months earlier, in a design office, a factory and a shipping schedule, and it is still running after the last module is lifted.
Why use modular construction for Australian housing?
Because the housing target is large and the clock is running. The National Housing Accord target is “1.2 million new homes by 2029”, and modular moves a large share of the work into a factory that builds while the site is still in foundations.
Government money is now behind it. The 2025-26 Budget committed $39.3 million to Advancing Prefabricated and Modular Construction Projects, $15.0 million in FY27 and $24.3 million in FY28, paid to participating states to build more homes with these methods. Federal and state building ministers agreed to cut red tape for the sector, and the Australian Building Codes Board released a Prefabricated, Modular and Offsite Construction Handbook on meeting the National Construction Code with offsite methods.
The supply chain is moving too. Prefab and modular building imports reached a record A$326.4 million in the year to November 2025, up 51.1%, with mainland China supplying 66.1% (Wood Central). The data does not separate housing from commercial and industrial buildings, so it shows supply growing, not homes completed.
What nobody can tell you is how much housing is actually built this way. Prefabrication is put at 3 to 5% of Australian buildings, and Prof Mathew Aitchison of Monash University and the Building 4.0 CRC calls that figure a guess, because no one systematically collects the data (Build Australia).
Why is modular established in mining and process plant but not in housing?
Because resources projects often have no other way to build. Remote sites, tight footprints and short installation windows forced the industry to build in yards and ship to site, and its programs have been built around that for years.
Gorgon LNG on Barrow Island is the benchmark. Hatch reports that 51 process modules and 236 pre-assembled racks and units, more than 240,000 tonnes in all, were built in fabrication yards in Asia and shipped to the island. The heaviest module weighed 6,300 tonnes. The project went modular because of its limited construction footprint, its remoteness and the island’s quarantine requirements as a Class A Nature Reserve.
The same factory and site logic now runs through modular process plant, skid-mounted equipment, prefabricated pipe racks and accommodation camps across mining and heavy industrial work. On a remote site a missing module cannot be replaced quickly, so the logistics chain is scheduled as hard as the installation.
Residential has been here before and has not kept the lessons. In 2013, the nine-level One9 building in Moonee Ponds had its 34 apartments erected on site in five days, using Hickory’s Unitised Building system. More than a decade later, the tallest volumetric modular building in the country is still being set in Macquarie Park.
Aitchison’s explanation is that past experience with prefab has not been retained, so the same mistakes get repeated. The Productivity Commission’s February 2025 housing construction report named “slow uptake of digital technologies and modern methods of construction” as one of four key problems, and UTS commentary on the report warns that poorly managed innovation “can even increase costs and reduce quality and productivity”.
The method is proven. In housing, the program discipline that makes it work is still being learnt.
How do you phase modular installations?
In lots that match the installation sequence. A lot is the set of modules needed to install one floor, zone or stage, and each lot is scheduled as its own chain, from factory slot to crane hook.
Follow one lot for level 9 and the program looks like this:
Design freeze: the module design for level 9 is fixed. A change after this date hits production, not just drawings.
Factory slot: the manufacturer books production around its other projects. Miss the slot and the next one can be weeks away.
Production and factory inspection: framing, linings, wet areas, in-module services and, on some projects, the facade are completed and inspected before the modules are closed up.
Shipping and customs: sea freight, port handling and customs clearance, each with its own duration and risk.
Transport: oversize road transport with permits, escorts and approved travel windows, often at night.
Buffer: the lot waits its turn, at the factory, in storage or on site, ahead of the crane.
Lift: installation starts only when the lot is available and the site is ready: supporting works, access, crane setup and the required inspections complete. Module lifts stop in high wind, so lifting days, not calendar days, set the rate.
Release: connections between modules, facade joints and weatherproofing, and finishing below the installed floor are linked to that lot’s installation, not to a general completion date.
In the program, factory and site each carry their own WBS, linked through these delivery and installation milestones. Production ahead of site readiness creates storage. Production behind it leaves crews and cranes idle. The install sequence drives the production, packing and dispatch sequence, not the other way round. This is phased material procurement applied to whole building modules.
Where does factory delay hit the site critical path?
When the lot misses its planned lift date and the buffer or resequencing options cannot absorb the delay. Whether that delays completion depends on the remaining float and the downstream connections, testing and handover sequence.
Every step in that chain before the lift sits upstream of the site, and most of it sits with someone other than the head contractor. Each belongs in the program as an activity with an owner and a duration, so a delay shows its effect on installation and completion the day it appears, not the day the crane stands idle.
What are the trade coordination challenges in modular projects?
The trades are split between the factory and the site, and the interface has to fit first time. Factory work has to meet structure, risers, service connections between modules and weatherproofing built on site.
Interfaces between modules: structural, fire, acoustic and services connections made on site after each lift, by trades who follow the crane floor by floor.
Inspection and evidence hold points: what must be inspected or documented before modules are closed up and dispatched, and what is verified on site. Each hold point has an owner and is linked to the activity it releases.
Testing, commissioning and handover: services connected on site still need testing and commissioning floor by floor, and this tail often sets the completion date after the last lift.
How much schedule acceleration can modular construction yield?
As much as factory and site work genuinely run in parallel, and the program logic is the only reliable way to measure it. The saving comes from overlap. The cost comes from an earlier design freeze, factory lead time, shipping and inspection steps that move from site to factory.
Build both programs, conventional and modular, from the same scope and compare them to the same completion milestone, with consistent calendars and resource assumptions. A modular program that shows a saving only because the factory duration was assumed, not confirmed by the manufacturer, has not shown a saving at all. Test it with schedule risk analysis on the factory, shipping and installation durations before committing to a completion date.
Who carries the delay when a module lot misses its lift?
The contract decides who carries it. The program decides whether anyone can prove it. If the factory sits in the program as a single delivery date, nobody can show where the time went.
Picture the level 9 lot arriving two weeks late. The head contractor points at the integrator. The integrator points at the manufacturer’s slot. The manufacturer points at a design change after freeze. Each may be right, and on a program with one bar called “modules delivered”, none of them can be tested.
With the chain in the logic, every step has a planned date, an actual date and an owner. The delay shows where it started, how much buffer it consumed and whether it reached completion. That record is the starting point for forensic delay analysis when the argument starts.
What should you require from a modular partner’s program?
A program that shows the factory as logic, not a single delivery date. Ask for:
Production schedule by lot: factory start, production and inspection for each lot, linked to the installation it supports.
Design freeze date: the date after which a change affects production, and the process for a change after it.
Logistics chain: shipping, customs, transport and permit activities with durations, for offshore and onshore supply.
Installation rate basis: the stated lifting rate, crane availability and the weather allowance behind it.
Buffer and storage plan: how many lots are held ahead of installation, and where.
Completion tail: connections, testing, commissioning and handover after installation.
Program integration: activity-level logic and progress data, with native Primavera P6 files where required for integration into the master schedule.
A partner who can provide these has a delivery program. A partner who can only provide a delivery date is asking the project to carry their risk.
Project Scheduling builds and reviews programs for construction, mining and heavy industrial projects across Australia in Primavera P6, including modular and offsite delivery, from tender program development through to schedule risk analysis and delay analysis. That includes construction scheduling in Melbourne, where One9 showed what offsite methods can do, and construction scheduling in Perth for remote WA resources work like Gorgon.
Frequently asked questions
What is modular construction scheduling?
Modular construction scheduling joins factory production and site works in one program. Modules are built and fitted out in a factory while site works proceed, so design release, factory production, logistics, site readiness and installation can each drive completion.
How do you phase modular installations in a phased project?
Deliver modules in lots that match the installation sequence. Schedule each lot as its own chain from production to installation, link each installation to both module availability and site readiness, and hold a buffer of lots ahead of the crane, at the factory or in storage where the site is tight.
How much schedule acceleration can modular construction yield?
It depends on how much factory and site work genuinely run in parallel. Compare a conventional and a modular program built from the same scope to the same completion milestone, with factory durations confirmed by the manufacturer, and test the result with schedule risk analysis.
What are trade coordination challenges in modular projects?
Trades are split between the factory and the site. Connections between modules, inspection and evidence hold points before dispatch and on site, and testing and commissioning after installation must all be scheduled so that factory work and site work meet first time.
What should a modular construction partner's program include?
A production schedule by delivery lot, a design freeze date, shipping, customs and transport activities, the basis of the installation rate, a buffer and storage plan, connections, testing and commissioning after installation, and progress data that can be integrated into the master schedule.
